Valphira is not a pure production service provider with external analytics. Valphira is a actual pharmaceutical manufacturer.
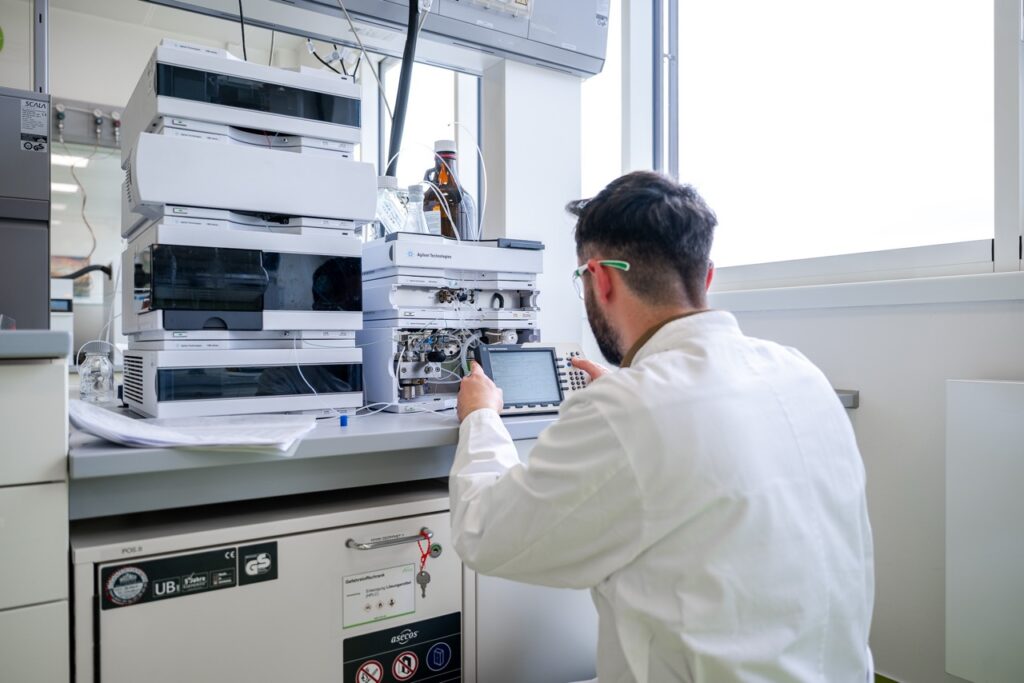
For us, this includes much more than just manufacturing: a high-performance GMP laboratory, sound analytical expertise, and a deep understanding of pharmaceutical quality are an integral part of our DNA.
Our laboratory is therefore not just a controlling unit at the end of a process. It accompanies the entire product lifecycle – from the starting material through in-process and release analytics to stability studies and methodological questions. This is precisely what creates the safety, depth, and professionalism expected of a modern pharmaceutical manufacturer.
Anyone who wants to produce solid dosage forms at a high level must master quality from the outset.
Therefore, Valphira not only tests finished products but also starting materials and stability samples according to pharmacopoeias (such as Ph. Eur. HAB) and other binding regulations. .
Our laboratory is designed to handle analytical questions across the entire value chain – traceable, documented, and GMP-compliant.
Our laboratory landscape covers a broad spectrum of chemical-physical, spectroscopic, and pharmaceutical-technological testing methods. These include, among others:
Thin-layer chromatography
A strong laboratory doesn't end with routine testing.
Valphira also accompanies Stability studies, in-use studies, photostability studies, and method transfer and validation.
Additionally, we want our Competence in the area of method development continue to expand in a targeted manner – with the aim of reliably supporting customers even with new or more demanding analytical questions.
This creates an environment that is suitable not only for established products but also for companies that want to introduce new products, transfer existing manufacturing processes, or professionalize their analytical basis.
In addition to classic pharmaceutical issues, Valphira possesses extensive expertise in the analytics of:
Experience is particularly valuable in these areas because products, raw materials, and analytical requirements are often more specialized than with standardized formulations. Our clients benefit here from a team that not only knows methods but also understands the specifics of the respective product world.
Our laboratory operates based on clear GMP principles. These include:
This is supplemented by sampling in a qualified cleanroom and environmental monitoring, including airborne microbes, surface monitoring, and airborne particles.
This is not an added benefit for us; it's a fundamental requirement. Because anyone who wants to reliably produce solid dosage forms needs not only good equipment but also a laboratory that provides robust confirmation of results and systematically ensures quality.
The Valphira Lab makes visible what we stand for as a company: pharmaceutical depth, analytical diligence, and genuine manufacturing responsibility.
This is a key reason why Valphira is able to professionally support and manufacture a very broad spectrum of solid dosage forms. Because the Ability to handle tablets, film-coated tablets, capsules, or other solid dosage forms safe to produce, relies not only on machines – but on Quality systems, methodological competence, experience, and clean analytics.
Valphira connects Manufacturing and Laboratory to an integrated overall pharmaceutical understanding. This is precisely what makes us a high-performing partner for solid dosage forms.